Product Description
Product details
| Country of Origin | Made in India |
| Model Name/Number | PURE H20 |
| Automation Grade | Automatic |
| Brand | Pure H2O |
| Material | Stainless Steel |
| RO Capacity | 500-1000 (Liter/hour) |
| Usage/Application | Industrial |
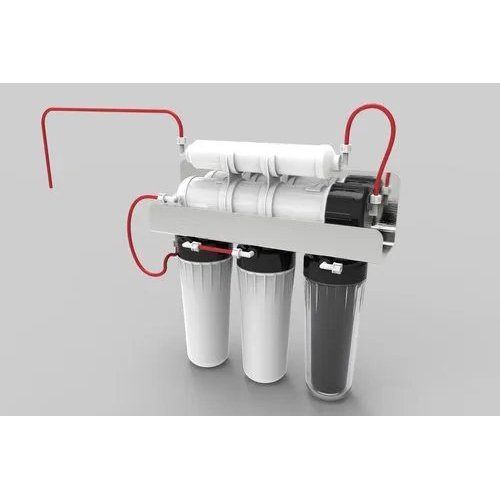
Advanced Control and AutomationEquipped with a PLC-based automatic control panel, the 500 LPH SS RO Plant offers seamless and intelligent operation. Users benefit from automatic shut-off features and digital displays, ensuring precise system monitoring of conductivity, TDS, and pressure in real time. The plant's stainless steel build and fully automatic grade allow for hassle-free, reliable water purification with minimal manual intervention.
Superior Water Purity and EfficiencyThis RO plant delivers exceptional water quality with a TDS rejection rate of up to 98% and a water purity level reaching up to 99%. Using leading-brand imported membranes and a robust multi-stage filtration process, it consistently produces safe potable water suitable for applications in drinking, food & beverage, pharmaceuticals, and industrial water treatment. The system is designed to work efficiently with inlet pressures of 1-4 kg/cm2.
Versatile and Customizable DesignFabricated from corrosion-resistant stainless steel and supplied as a skid-mounted unit, this plant is ideal for diverse environments. Its dimensions are customizable to suit specific site requirements, and the system supports a wide variety of raw water sources, including borewell, municipal, and well water. Onsite after-sales service support ensures ongoing reliability and user satisfaction.
FAQ's of 500 LPH SS Ro Plant:
Q: How does the PLC-based automatic control enhance the operation of this 500 LPH RO Plant?
A: The PLC-based automatic control panel manages all vital operations such as pump regulation, membrane cleaning, and safety protocols with minimal human input. This system ensures reliable water quality, efficient energy usage, and immediate automatic shut-off during abnormal conditions, reducing downtime and maintenance needs.
Q: What types of water can this RO plant treat, and what is its main application?
A: The plant is engineered to process a wide variety of water sources, including borewell, municipal, and well water. Its main applications cover drinking water supply, food and beverage production, pharmaceutical use, and industrial process water treatment where high purity and consistent flow are essential.
Q: When is maintenance required, and how easy is it to maintain the plant?
A: Routine maintenance is minimal due to the plant's corrosion-resistant stainless steel construction and robust filtration system. Routine checks typically include filter replacement and membrane cleansing, with the online chemical dosing system simplifying membrane protection. Schedule maintenance is further supported by digital system alerts and onsite after-sales assistance.
Q: Where can this RO plant be installed, and is it adaptable to space limitations?
A: The skid-mounted, customizable design allows for installation in a variety of locations, including industrial units, commercial establishments, and remote sites. Its dimensions can be tailored to the customer's available space, making it adaptable for areas with specific installation requirements.
Q: What is the process flow in this RO system?
A: Raw water first passes through sand and activated carbon pre-filters to remove suspended particles and organic impurities. It then moves through imported leading-brand RO membranes for high-efficiency purification. Online chemical dosing protects the membrane, and the digital display provides operational data. The final output is water with up to 99% purity and low conductivity.
Q: How does the plant ensure user safety and product longevity?
A: The system incorporates both low and high-pressure switches and automatic shut-off mechanisms, preventing operational errors and potential damage to key components. The stainless steel construction, combined with digital monitoring and efficient membrane cleaning, ensures longevity and continued safe operation in demanding environments.
Q: What benefits does this plant offer over conventional water purification units?
A: It delivers higher efficiency (up to 98% TDS rejection and 99% purity), lower noise, minimal user intervention, customizable configuration, and onsite after-sales support. This translates to operational cost savings, consistent water quality, and enhanced equipment durability for the end user.

 Get a Quote




 Send Inquiry
 Send Inquiry
 Send SMS


 English
 Spanish
 French
 German
 Italian
 Chinese (Simplified)
 Japanese
 Korean
 Arabic
 Portuguese
