Product Description
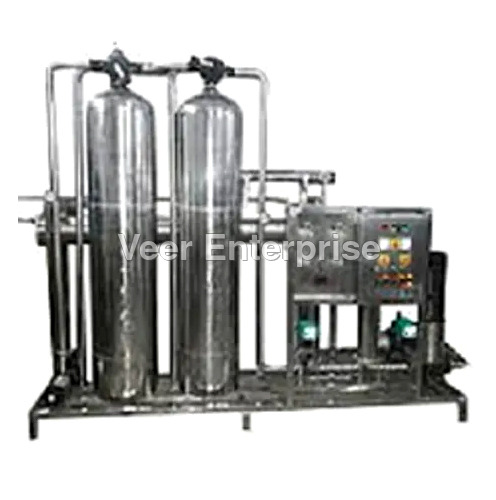
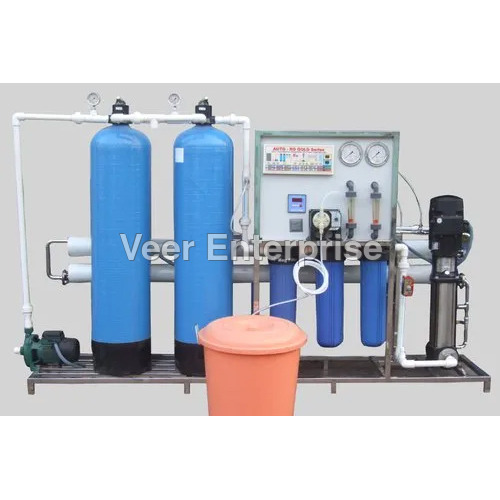
The 500 LPH Industrial RO Plant is a top-ranking, hot-selling solution for diverse industrial water purification needs. Designed with brilliant reverse osmosis technology and excellent features, it promises up to 99% TDS reduction and efficiency up to 99%. The system offers customisable membrane configurations (2-4 TFC spiral wound polyamide membranes) and advanced PLC/digital control with auto shut-off and alarms. This in-demand plant boasts robust SS 304/316 construction, CIP cleaning, and superb salt rejection (>96%). Capitalise on its low energy usage (2-3 kW), corrosion resistance, and adjustable automation for cutting-edge, reliable performance.
Versatile Usage and Wide Applications
The 500 LPH Industrial RO Plant is extensively used by industries seeking reliable large-scale water purification. Ideal for applications such as food & beverage, pharmaceuticals, boiler feed, textiles, and commercial establishments, it delivers consistent output and superior purity. Its excellent adaptability makes it suitable for borewell, tap, river, or industrial water, providing flexibility across different operational needs. The advanced design and fully automatic operation ensure convenience for both continuous and batch processes.
Order, Shipping and Sample Availability
FOB port services ensure streamlined, on-time delivery from India, allowing customers to expedite procurement. Sample units are available for evaluation, supporting quality assurance before finalising orders. The plant's completion rate and shipped goods efficiency reflect strong manufacturing capacity and prompt dispatch-delivery typically occurs within a defined timeline post order confirmation. This reliability, coupled with a responsive order tracking system, guarantees you capitalise on uninterrupted operations and superior customer support.
FAQ's of 500 LPH Industrial RO Plant:
Q: How does the 500 LPH Industrial RO Plant achieve such high TDS reduction?
A: The plant employs advanced TFC spiral wound polyamide membranes and multi-stage filtration, enabling it to achieve up to 99% TDS reduction and over 96% salt rejection, ensuring exceptional water purity.
Q: What types of water sources can this RO plant treat?
A: It is engineered to handle borewell, tap, river, and industrial water sources, offering impressive versatility for various operational environments and applications.
Q: Where can the 500 LPH Industrial RO Plant be installed?
A: This unit is suitable for installation in industrial facilities requiring water for purification, food & beverage processes, boilers, pharmaceuticals, textiles, and commercial complexes, either skid-mounted or floor-mounted as per site requirements.
Q: What is the process for cleaning and maintaining the plant?
A: The system includes an integrated CIP (Clean-In-Place) facility, enabling automatic, hassle-free membrane cleaning without dismantling, ensuring sustained operational efficiency and membrane longevity.
Q: How long does delivery take after order completion?
A: Typically, goods are shipped promptly after order confirmation, with delivery times depending on the destination and order size, ensuring a dependable supply rate for your operations.
Q: What benefits does the built-in control panel offer?
A: The digital/PLC control panel with monitoring display allows easy management, real-time status updates, auto shut-off, alarms, and optimised plant performance, enhancing operational safety and efficiency.

 Get a Quote





 Send Inquiry
 Send Inquiry
 Send SMS
 Call Me Free


 English
 Spanish
 French
 German
 Italian
 Chinese (Simplified)
 Japanese
 Korean
 Arabic
 Portuguese
