Product Description
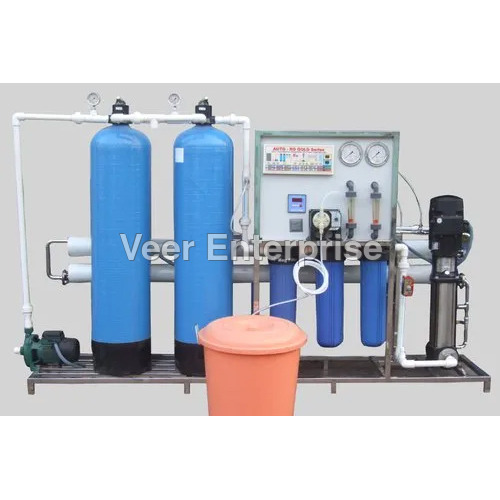
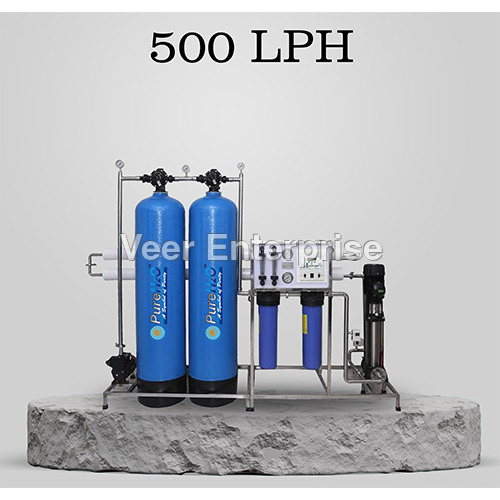
Discover the new, hot-selling 5000 LPH Industrial RO Plant, engineered with ultimate precision for cost-effective water purification in demanding industries. Featuring 4-6 matchless Thin Film Composite (TFC) membranes and a multi-stage pre-treatment process-multi-grade sand, activated carbon, and micron filtration-it delivers uncompromised purity up to 98%. The uncommon, rugged skid-mounted design uses mild steel powder coating for durability and offers a fully automatic, PLC/pneumatic/relay-based control system. Enjoy the benefits of a high recovery rate (60-70%), low power consumption, and CIP cleaning for superior operational efficiency and minimum maintenance.
Versatile Applications & Competitive Advantages
The 5000 LPH Industrial RO Plant is ideal for treating borewell, municipal, and industrial water, suitable for drinking, process, food and beverages, and pharmaceutical uses. Its primary advantages include an unmatched recovery rate, high efficiency of up to 98%, rugged construction, and complete automation. Used as a robust solution for diverse water treatment needs, it supports both small and large-scale industries with flexible, reliable performance in even the most demanding environments.
Robust Supply Ability & Sample Policy
We ensure quick dispatch with express shipping or secure shipping modes across India and globally. Our supply ability matches high-volume manufacturing needs with assured stock availability. Customers can request samples-subject to our sample policy-to estimate compatibility before bulk orders. Samples are available on request, allowing businesses to validate quality and performance with confidence before procurement, ensuring satisfaction and reliable commissioning of every industrial RO solution we provide.
FAQ's of 5000 LPH Industrial RO Plant:
Q: How does the 5000 LPH Industrial RO Plant ensure high water purity?
A: The RO plant uses multiple pre-treatment stages-including multi-grade sand, activated carbon, and micron filtration-followed by thin film composite membranes and post-treatment UV/UF. This multi-stage process ensures water purity up to 98% with conductivity below 20 S/cm.
Q: What are the key benefits of using this industrial RO plant?
A: Some primary benefits include robust construction, automated controls, high recovery and recycle rates, low power consumption, long membrane life, and minimal maintenance requirements, delivering unmatched cost-effectiveness and operational efficiency.
Q: Where can this RO plant be used for optimal performance?
A: This plant is best suited for industries needing large-scale purified water, such as food and beverages, pharmaceuticals, drinking water, process water, and other manufacturing sectors relying on dependable, continuous water treatment.
Q: What is the process for cleaning and maintaining the system?
A: The plant is equipped with a Clean-In-Place (CIP) system, allowing automated or manual flushing and cleaning of membranes, ensuring longer service life and consistent operation with minimal downtime.
Q: How can I sample or test the RO plant before placing a bulk order?
A: Samples are available upon request following our sample policy, allowing you to evaluate the system's quality and suitability for your application before making a large-scale investment.

 Get a Quote




 Send Inquiry
 Send Inquiry
 Send SMS
 Call Me Free


 English
 Spanish
 French
 German
 Italian
 Chinese (Simplified)
 Japanese
 Korean
 Arabic
 Portuguese
